Engine rebuilding starts with a block and heads carrying everything a service life deposits: rust, carbon, paint and grease, all of which must be completely gone before machining and inspection. This application study documents the single-tank ultrasonic process that replaces the hot tank, the bead blaster and most of the scraping bench.
The contamination
Rust through the water jacket
Corrosion scale in cooling passages no brush or blaster reaches — the soil that decides whether a rebuilt engine runs at temperature or above it.
Carbon and baked oil
Combustion-face carbon and galleries varnished with a service life of oil — the hot-tank soils, without the hot tank’s days-long soak.
Paint and gasket residue
Old paint and bonded gasket material that otherwise costs hours of scraping and abrasive attack on machined faces.
The process
| Parameter | Value |
|---|---|
| Chemistry | Heavy-duty alkaline deruster, 15–20% typical; as low as 7% proven in marine overhaul |
| Temperature | 70–80 °C |
| Frequency | 40 kHz |
| Cycle | 1–2 hours total wash time |
| After-treatment | Rinse + anti-rust dip inside the flash-rust window |
| Materials note | Ferrous only at this strength — aluminium components run an inhibited chemistry instead |
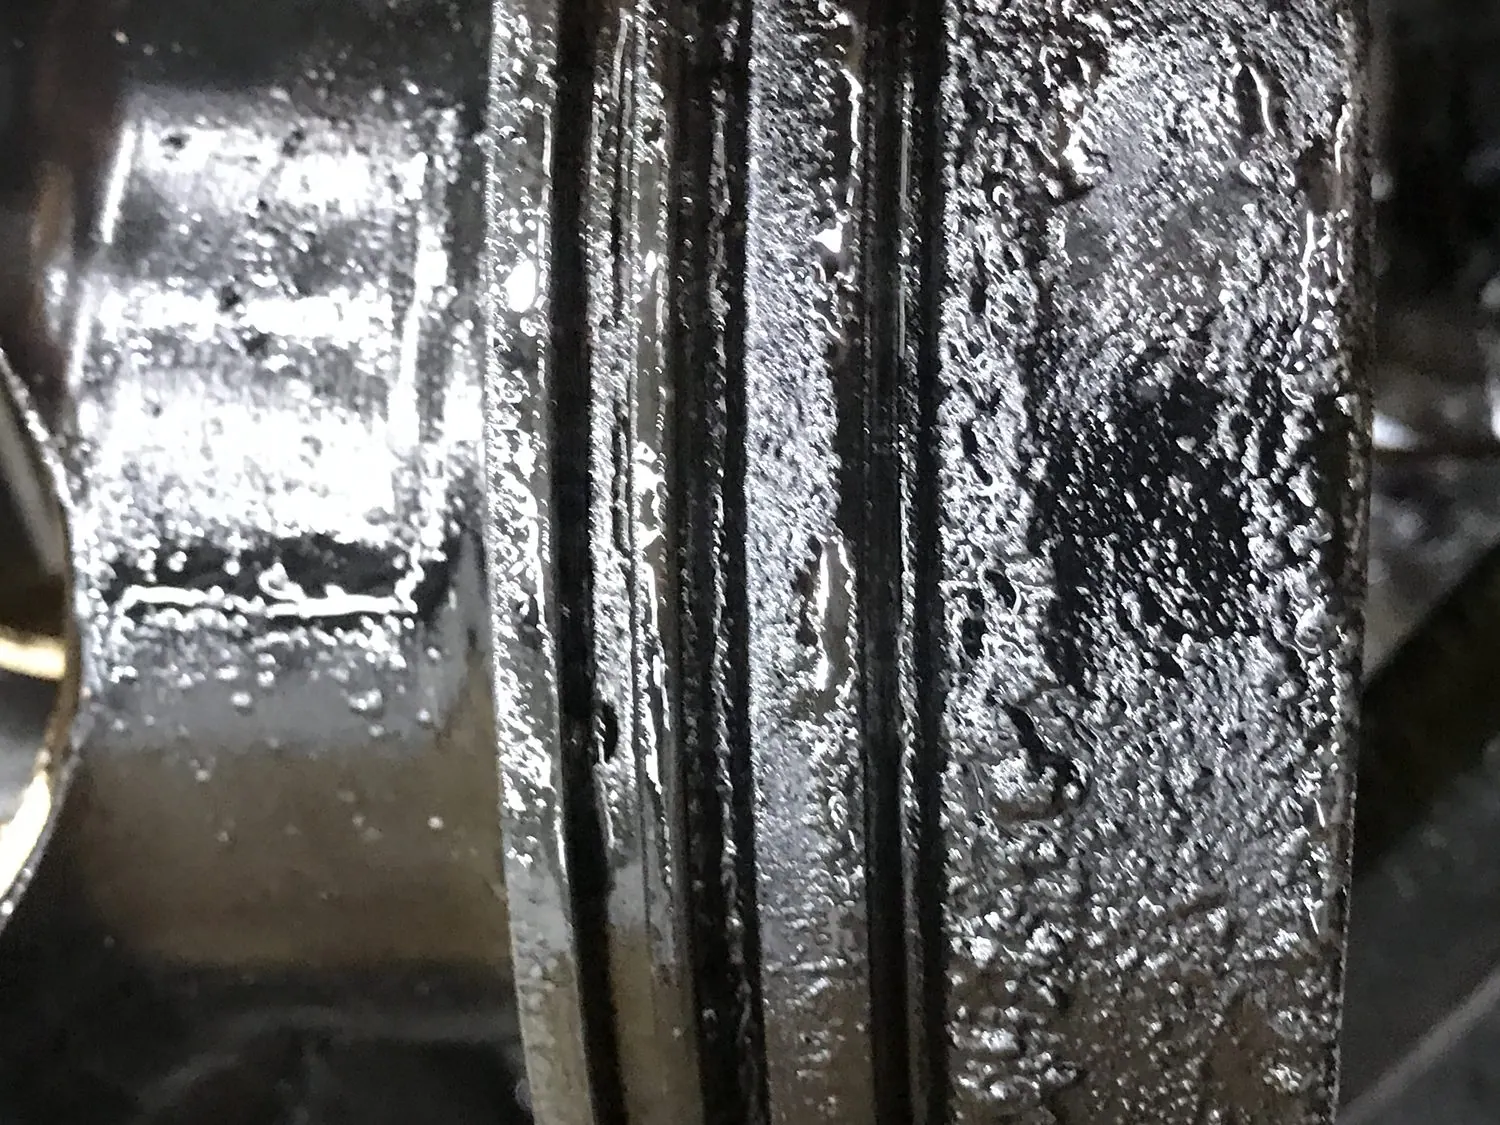
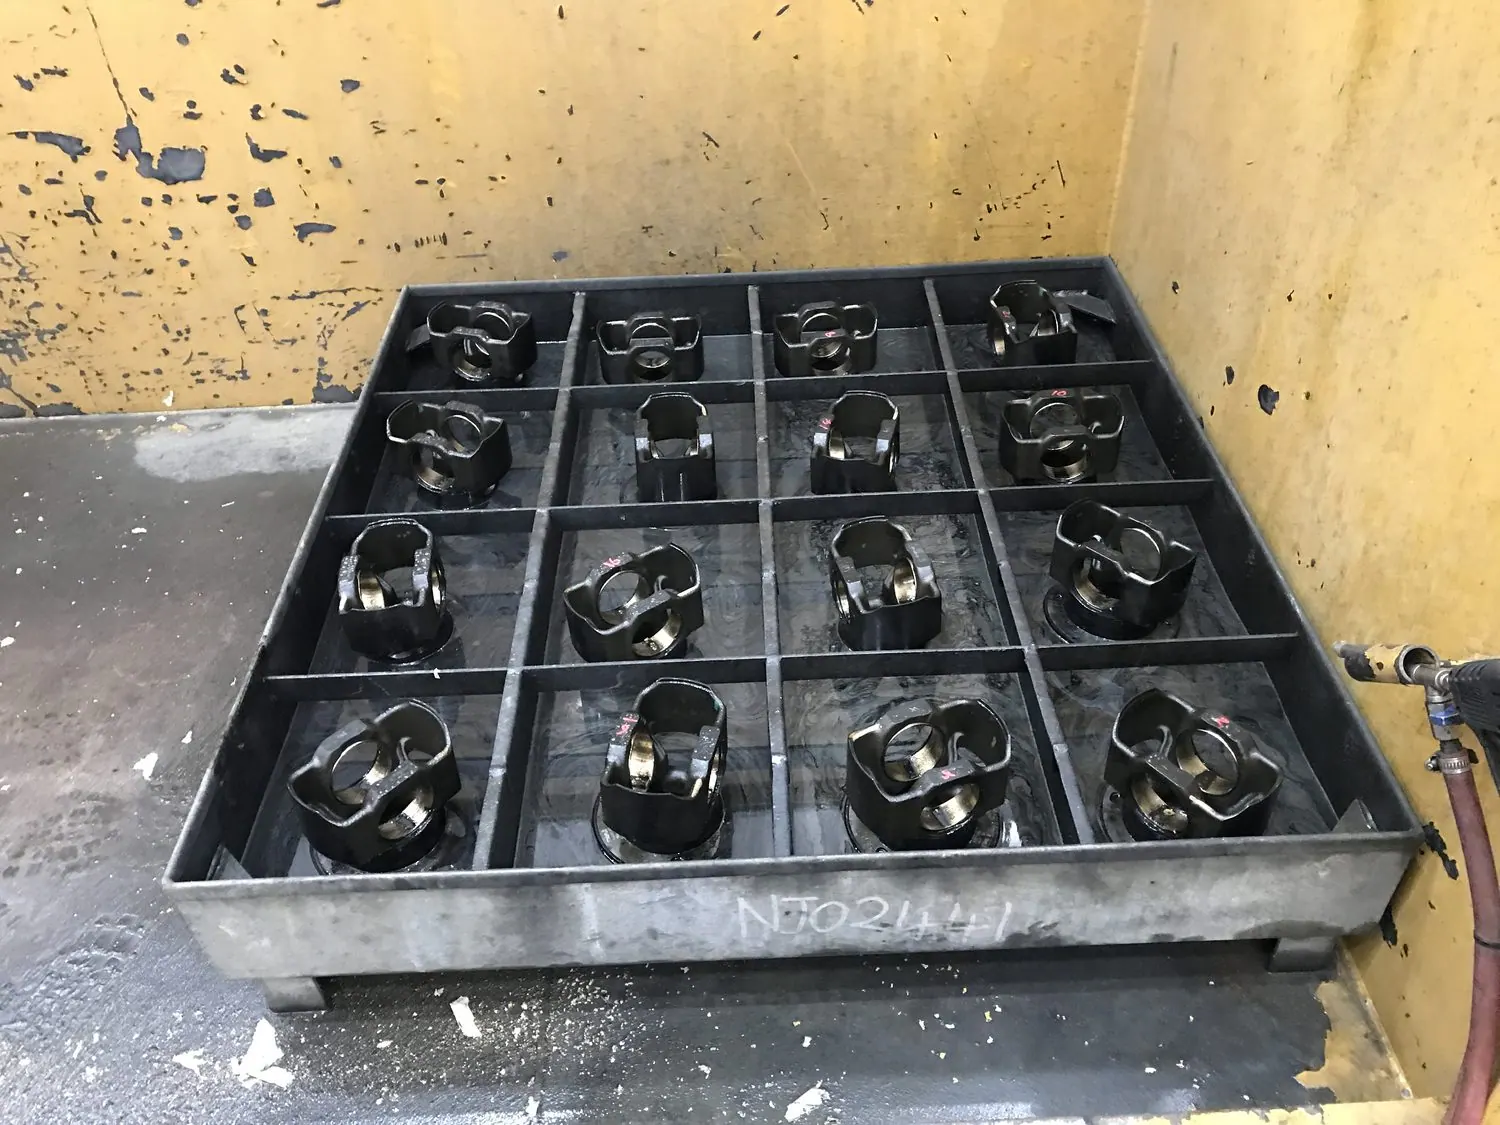
Piston skirt and crown. Baked carbon on the left, bare aluminium on the right — no bead blasting, no scraping, no dimensional change. Drag the handle across to compare.
The results
Hardware and chemistry
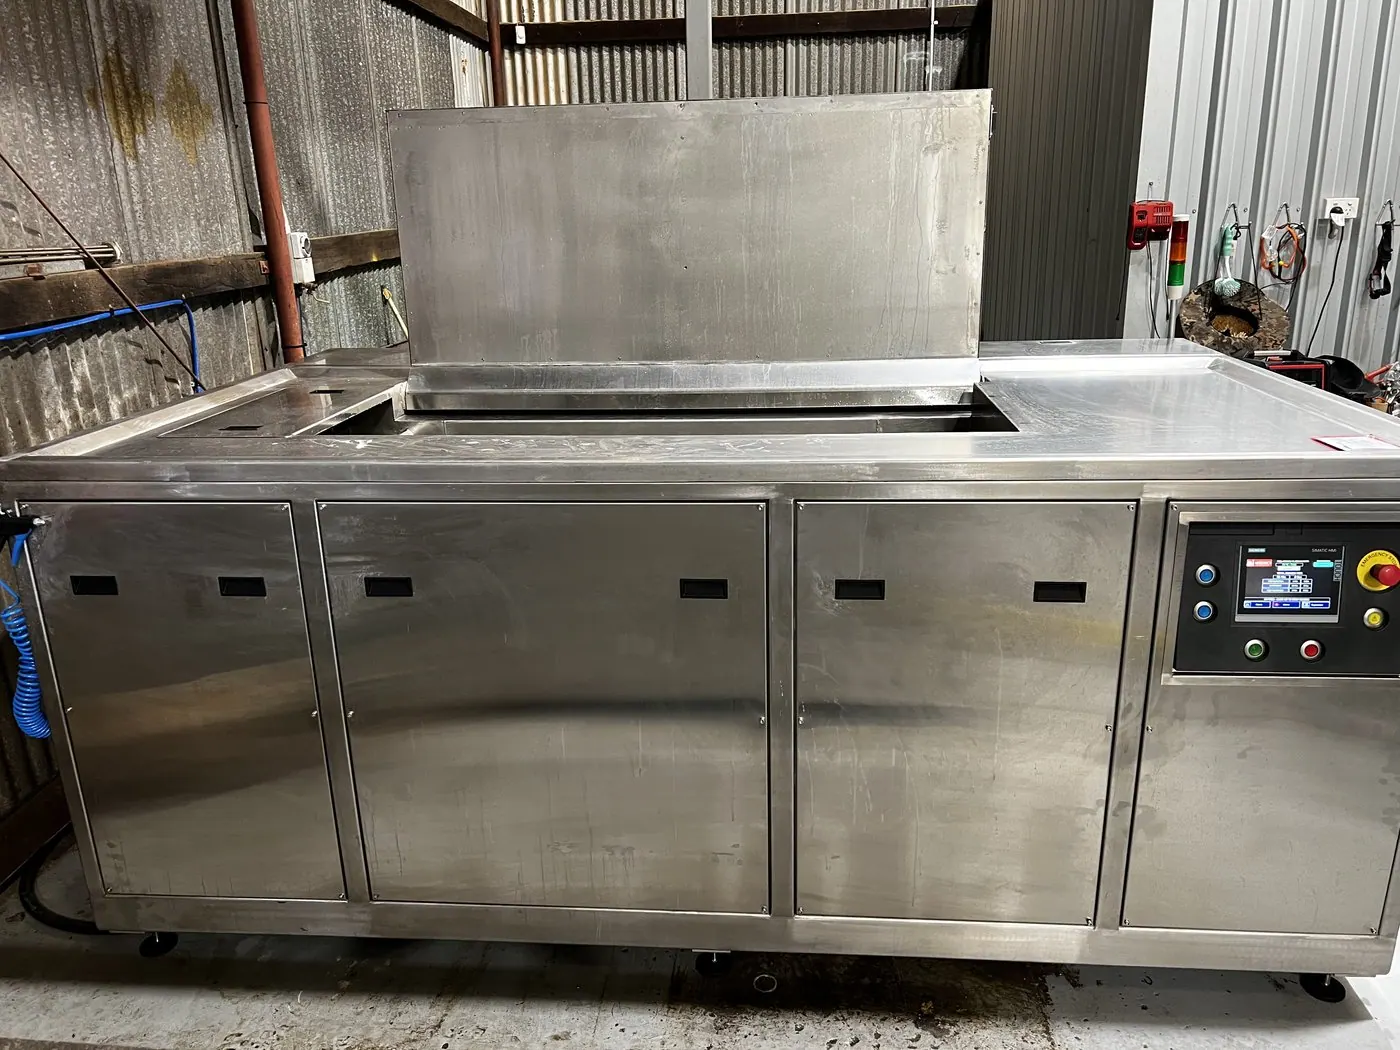
Heavy-duty industrial tank
40 kHz industrial tank with weir, filtration and a basket rated for block weights — sized to the largest engine in the program.
Ask about block-tank sizing →
Deruster chemistry
High-alkaline rust, carbon and paint stripper for ferrous rebuild work, paired with an anti-rust dip.
Browse the chemistry range →