Stainless steel is only stainless when its chromium-oxide layer is intact — and machining, welding and handling leave free iron that corrodes exactly where the certificate says it will not. This study documents the citric passivation route: NASA-validated as equivalent or better than nitric, conforming to AMS 2700 and ASTM A967, without the nitric acid handling burden — and the operating-cost workbook that quantified the switch.
The problem citric solves twice
Free iron contamination
Tooling and handling embed iron in the stainless surface; it rusts, stains and seeds pitting. Passivation dissolves it and lets the chrome-oxide layer reform — the whole point of the process.
The nitric burden
Traditional nitric passivation works — at the price of fuming acid handling, NOx exposure risk, neutralisation, disposal and the WHS file that follows it everywhere.
The evidence base
NASA’s published comparative studies found citric passivation equal or superior on the alloys tested — the reference that lets a quality system change without argument.
The process
| Parameter | Value |
|---|---|
| Pre-clean | Ultrasonic alkaline clean — passivation only works on a clean surface (ASTM A380) |
| Passivation | Citric acid solution |
| Rinse | DI water cascade |
| Verification | Per specification: water-break, ferroxyl or copper-sulphate test |
| Conformance | AMS 2700 (citric methods) · ASTM A967 · ASTM A380 practice |
The results
Hardware and chemistry
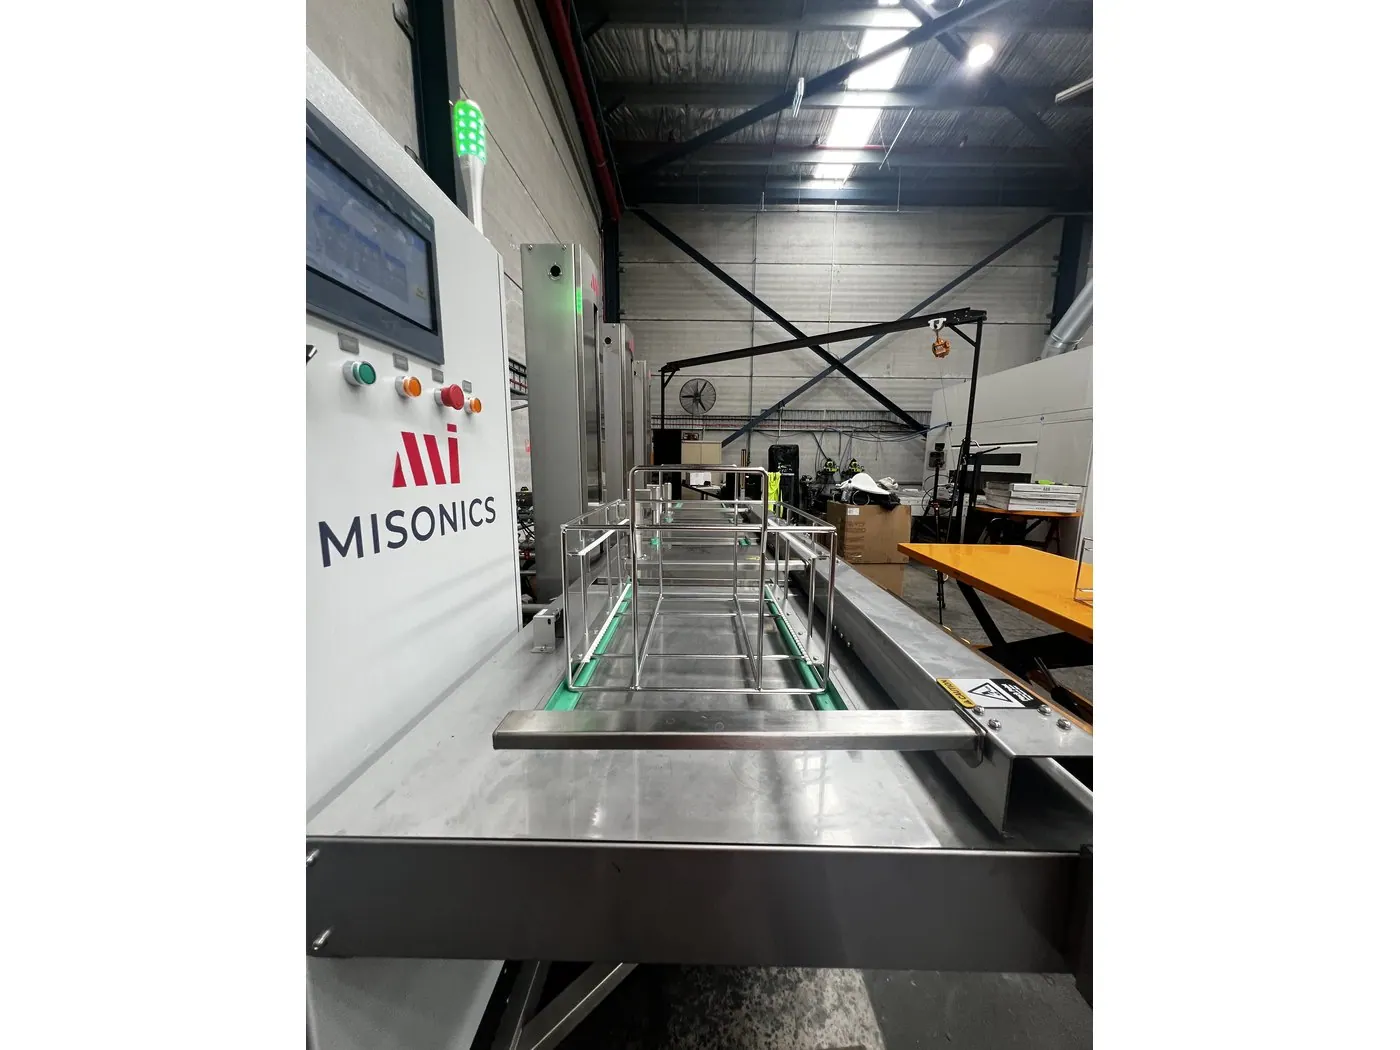
Passivation line equipment
Heated ultrasonic pre-clean, citric immersion and cascade rinse tanks — bench scale to production line.
Ask about passivation lines →
Passivation chemistry
Citric acid and the Brulin passivation range — specification-conformant products with the documentation to match.
View the passivation range →