The same element
Before and after
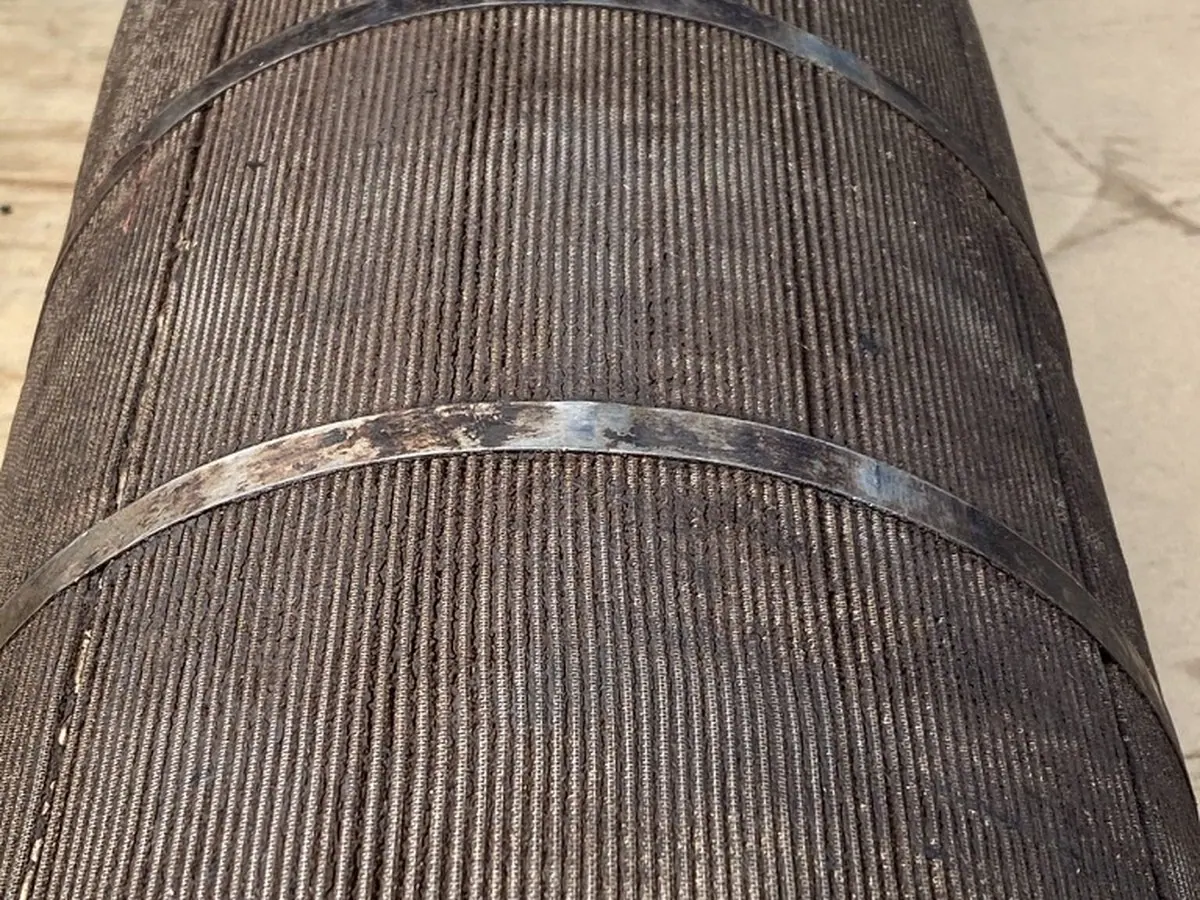
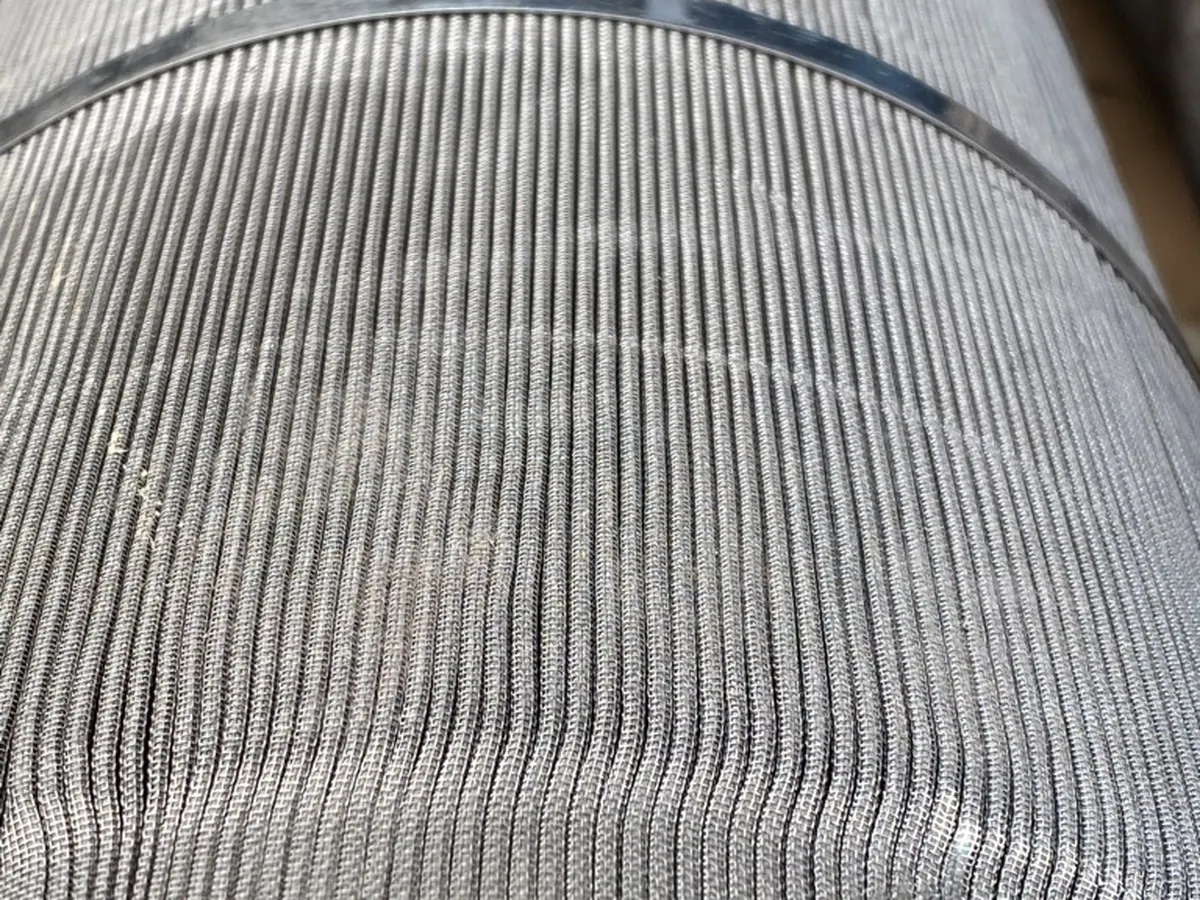
Pall pleated stainless mesh candle elements, blinded solid with carbonised process residue. Cleaned through the full depth of the pleat pack and put back in the housing.
MetalTek 100 is a strongly alkaline multi-soil cleaner for ferrous metals, rated 10–30% v/v at 60–80 °C with 80 °C the maximum. 25% at 75 °C sits in the middle of that window. The elements are stainless, so the ferrous-only restriction is not a constraint here.
One hour, one bath, no dismantling and nothing mechanical near the pleat pack.
Process figures as run. Your own will be set by a trial against your soil.
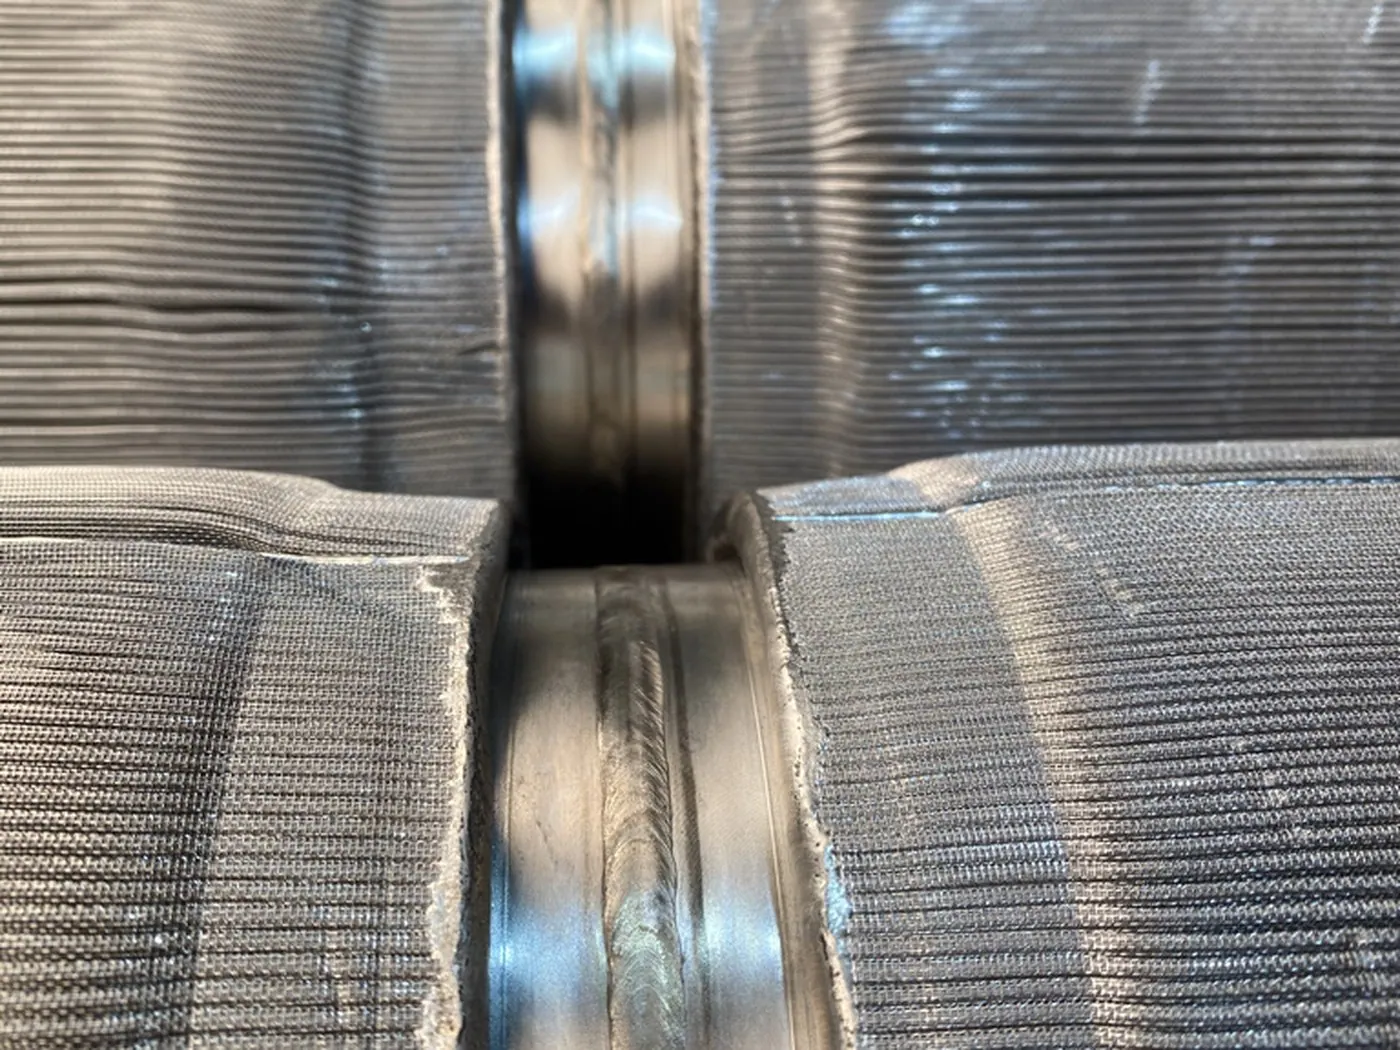
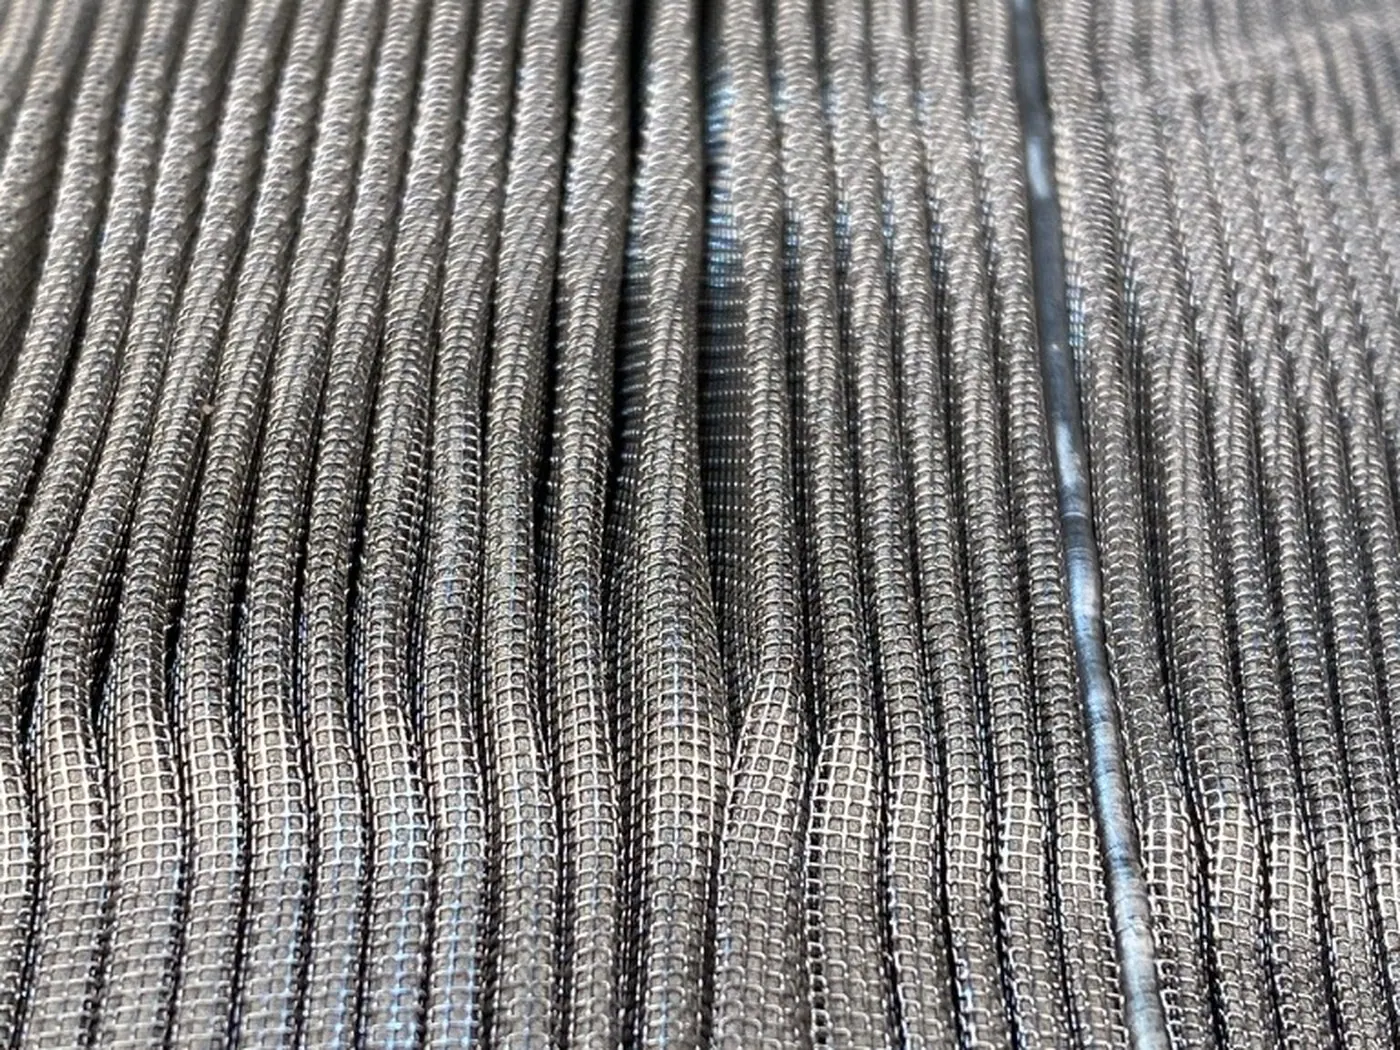
A pleated woven stainless wire cloth wrapped around a perforated stainless core, in segments, banded and welded, on a machined collar with a coarse male thread and a hex drive. The element screws into a tube sheet and hangs in the housing. It is built to be taken out, cleaned and put back — which is why it is worth cleaning.
The pleats are what make it hard. Pleating multiplies the filtering area inside the same envelope, and every fold is a pocket. Solids pack into the root of the fold where nothing can reach them mechanically. The outer face can look serviceable while the pack behind it is solid.
The deposit on these was dark and hard — carbonised, not loose sludge. It had bonded to the wire rather than sitting on it.
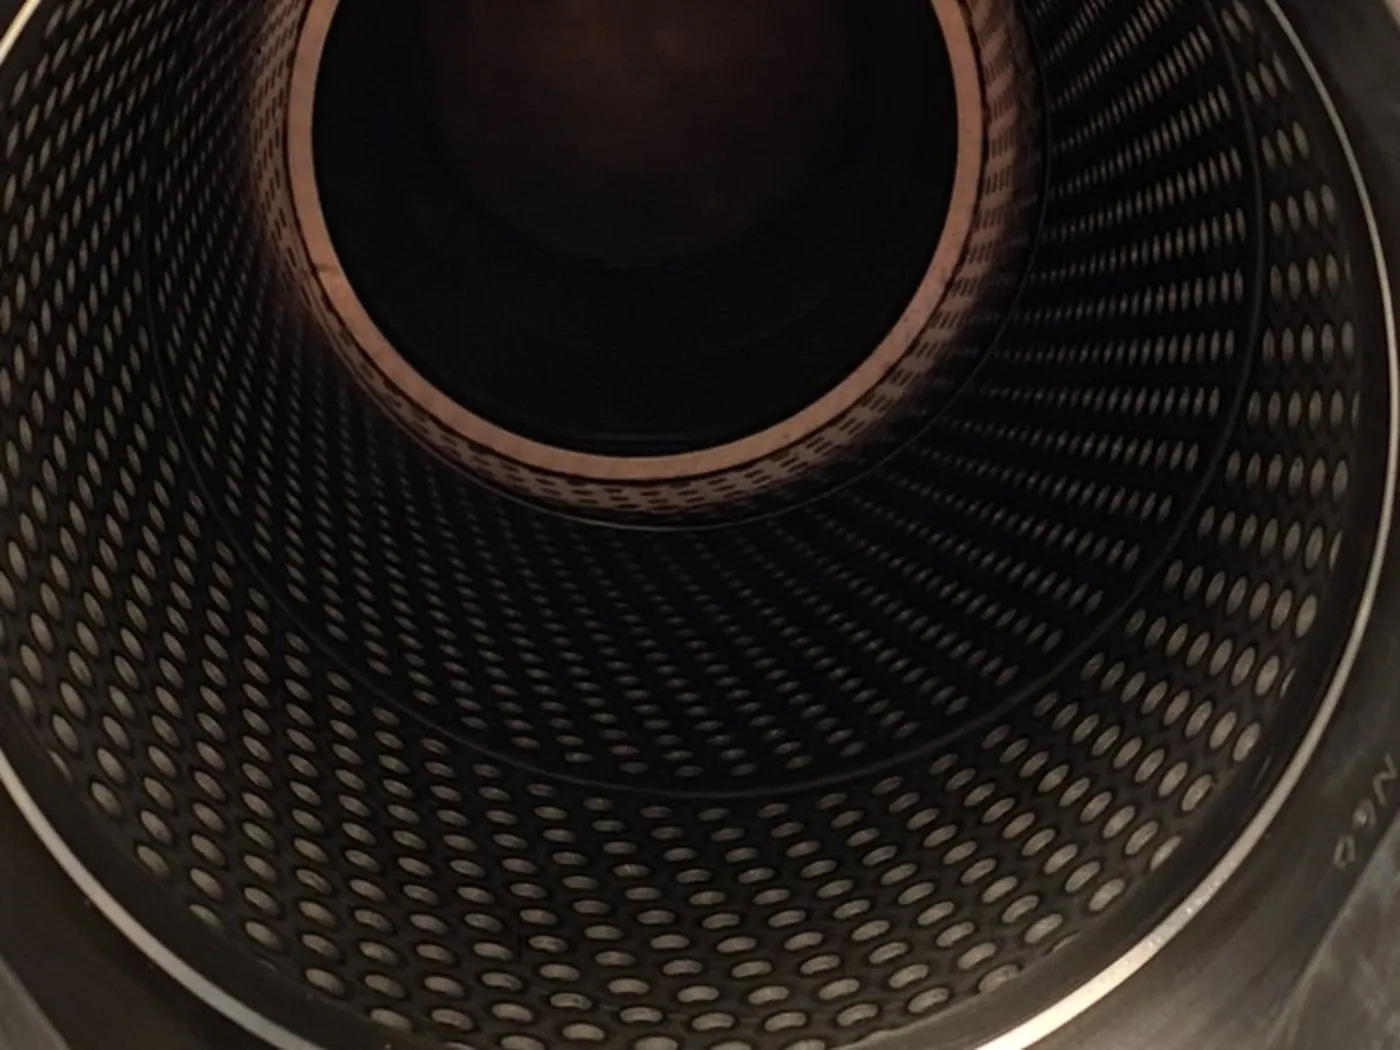
These housings are designed to backwash in service, and a backwash works well on the solids it was designed for — loose cake, sitting on the upstream face, released by a pressure reversal.
It does nothing about the other kind. Once the deposit carbonises or polymerises, it stops being cake and becomes coating. It is bonded to the wire and it is inside the fold. Reversing the flow pushes on it and it does not move. Differential pressure climbs cycle after cycle, the backwash interval shortens, and eventually somebody writes a purchase order for a new set.
Ultrasonic cleaning works on a different principle. Cavitation happens wherever the liquid wets, so it reaches into the fold root and the core perforations at the same rate as the outer face. There is no line of sight to lose and no pressure to direct. Matched chemistry softens the bond; the cavitation takes it off the wire.
It is also gentle on the element in a way nothing mechanical is. Nobody brushes a pleat pack or runs a lance down it without closing pleats and opening others. A blocked pleat is a lost rating; a stretched one is a bypass. Immersion touches nothing.
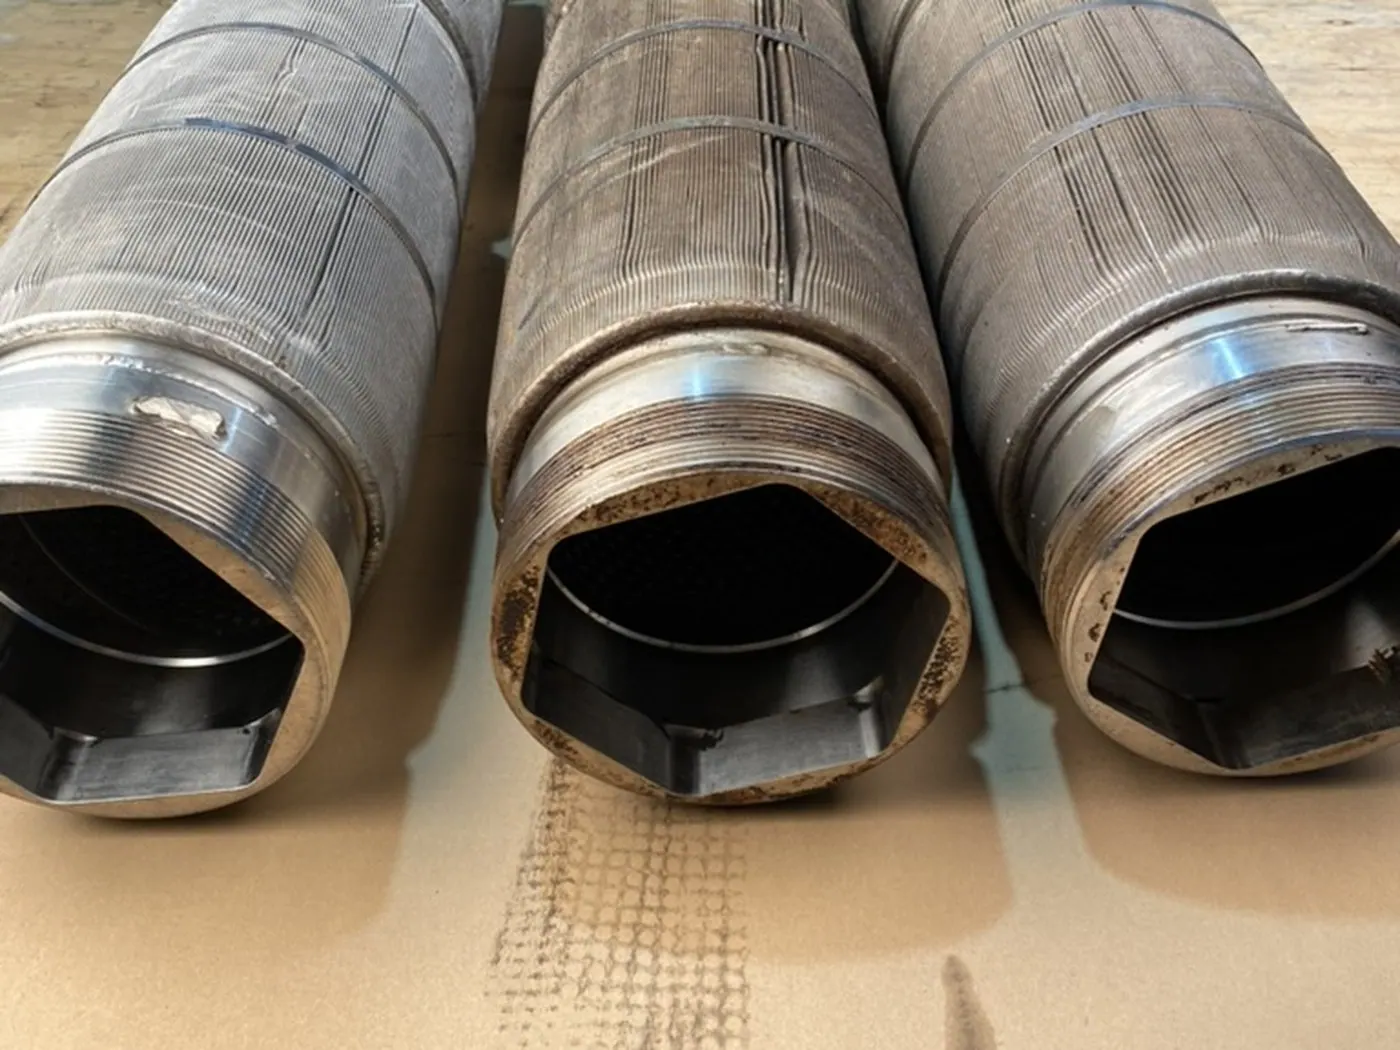
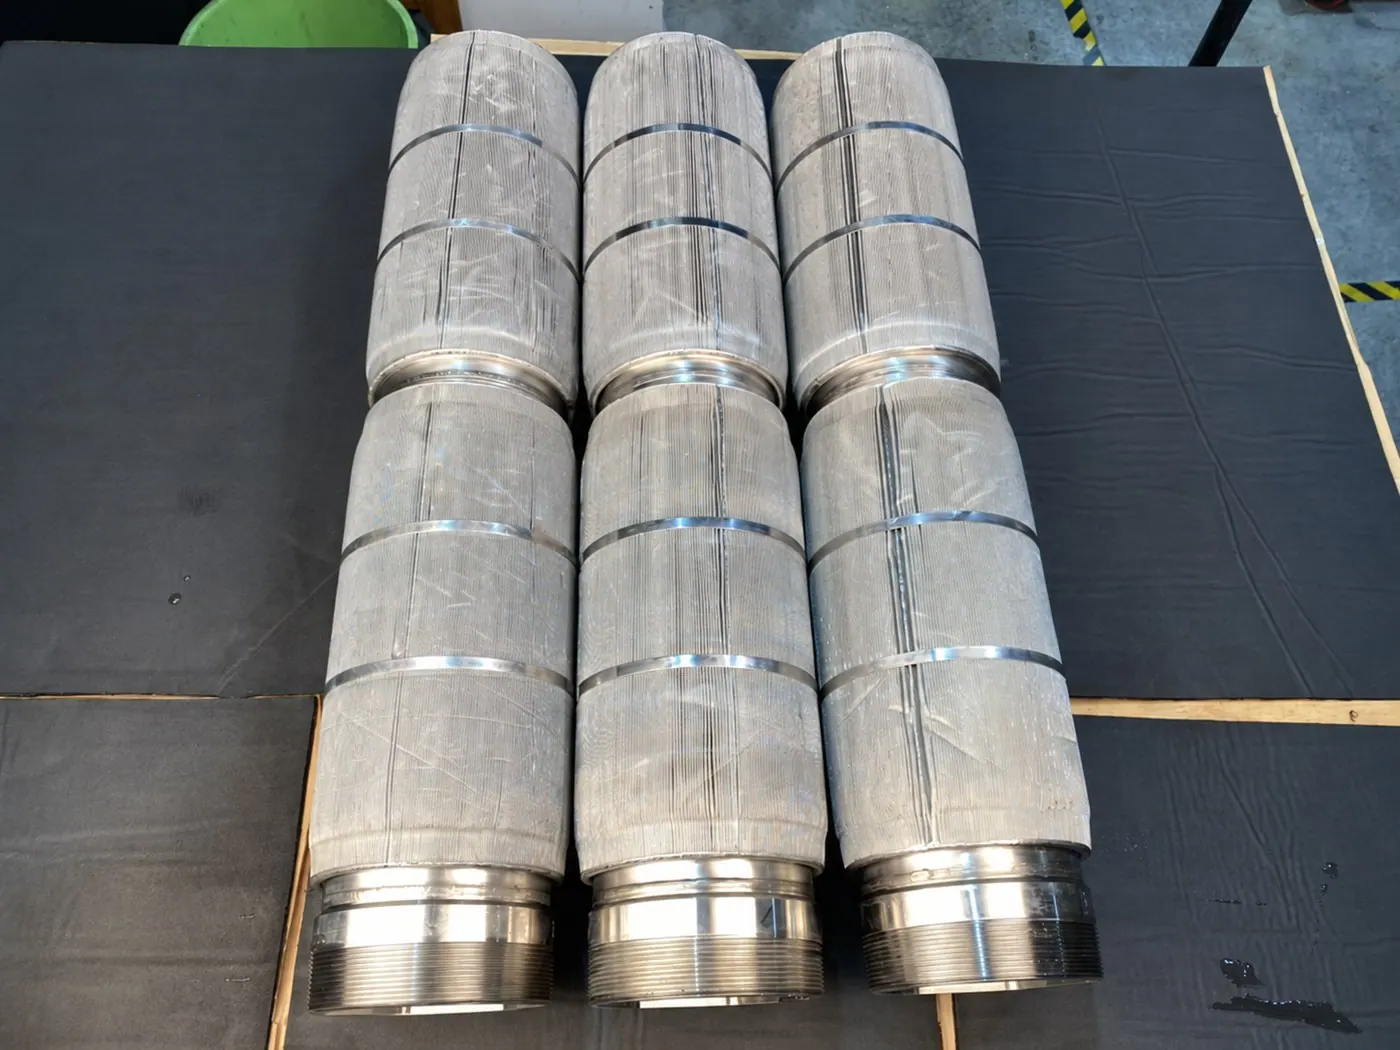
The machined collar and the thread come up as well as the mesh. That matters: the collar is the seal into the tube sheet, and residue on a sealing face is a bypass that no element rating can fix.
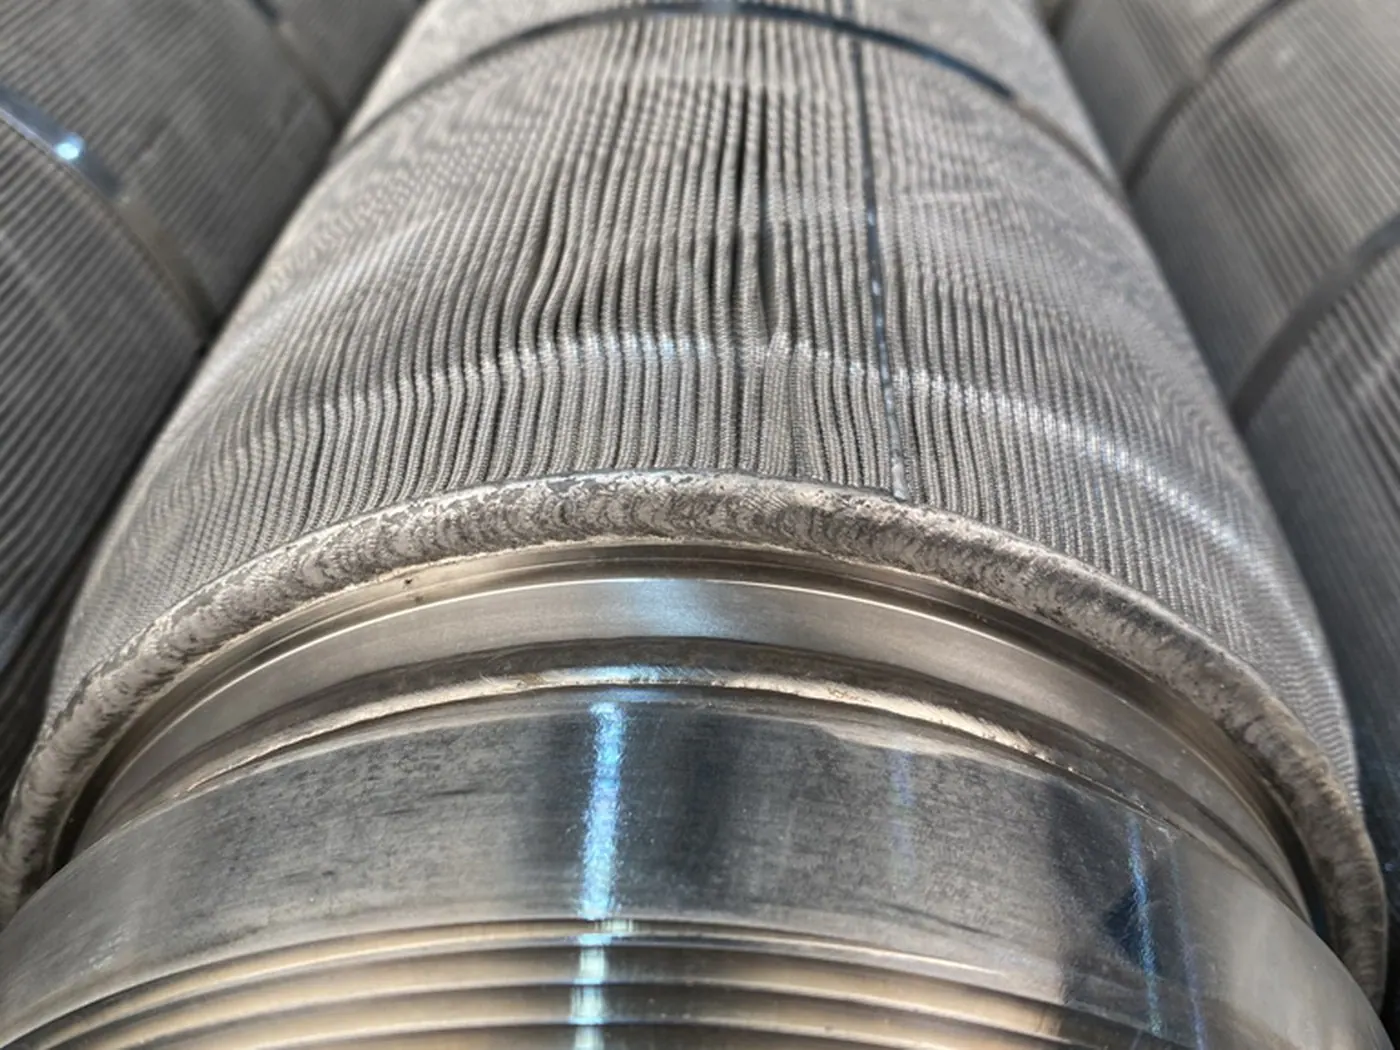
A pleated mesh candle element is an engineered part. It is laser-welded stainless, machined, and on a long lead time from overseas. A housing holds several, and they are replaced as a set. That is what makes the sum worth doing.
Four numbers decide it, and they are all yours rather than ours:
Cleaning does not beat replacement every time. It beats it when the element is expensive, the lead time is long, and the fouling is the bonded kind a backwash was never going to shift. On that set, it usually is not close.
There is a limit and it is worth saying. Cleaning recovers an element that is sound. It does not repair one. A holed pack, a crushed pleat, a cracked weld or a damaged sealing face is scrap, and we will tell you that rather than hand it back looking clean. Elements come back with what we found noted.
Element length picks the machine, not element count. A candle has to lie or stand in the bath with liquid all round it, so measure the longest element in the housing and work from there. Everything below is a heated immersion tank with the chemistry, filtration and oil separation sized to the soil.
Not sure which? Send the element length, the outside diameter across the pleat pack and how many are in the housing. That is enough to name the machine.
Tell us which elements you are replacing, how often, and what service they come out of. Technical sales will tell you whether cleaning is the right answer for that fouling, and what it takes to do it on your own floor — the machine, the chemistry and the cycle.
Where that conversation shows a trial is genuinely needed, we write a trial protocol with acceptance criteria, quote it, run it and give you the report. The cost of the trial is credited in full against the machine.
Related: EvoSonic EVS 300 · Power plant component cleaning · All case studies